
Industries / Pharma & Sciences
Pharmaceutical Supply Chain Consulting
Scale supply. Keep control.
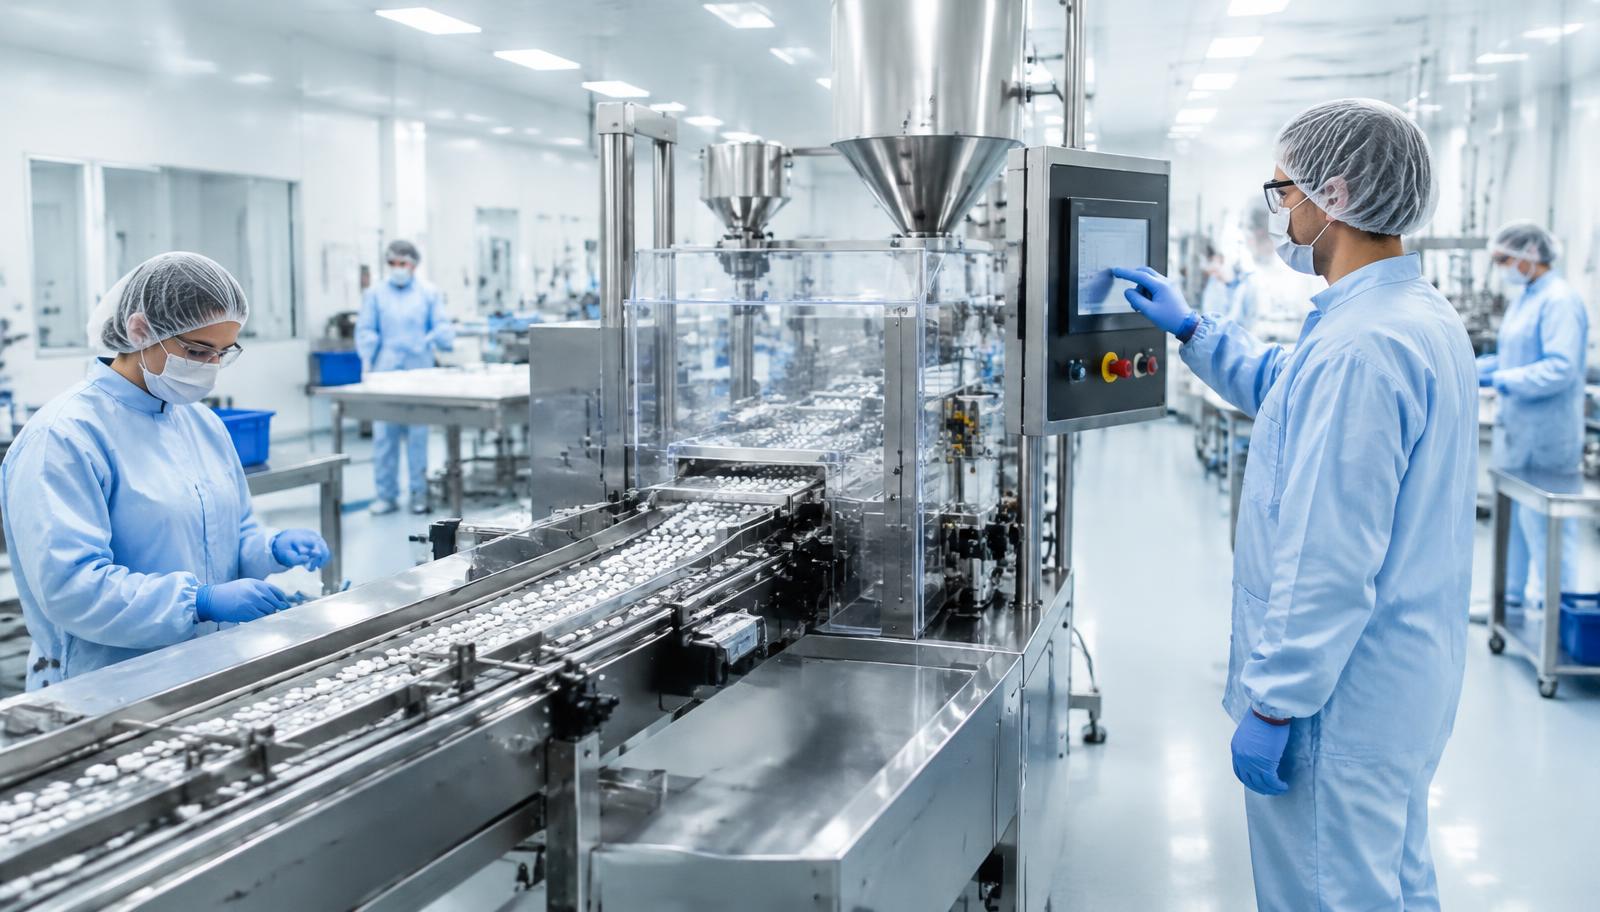
Most pharmaceutical plants make more batches than they can ship on time. The gap sits between product manufactured and product cleared to ship: testing queues, documentation review and quality release. Maine Pointe provides pharmaceutical supply chain consulting, pharmaceutical manufacturing consulting and strategic sourcing consulting that closes that gap, so more of what you make reaches patients by the promised date without compromising quality or margin.
10–45%Competitive gap closed for a generic pharmaceutical manufacturer through supplier qualification, procurement routines and staff training
10%profitability improvement
In short
Maine Pointe provides pharmaceutical supply chain consulting that protects supply and margin through supplier qualification, procurement discipline and release capacity. We help manufacturers close competitive cost gaps without putting compliance at risk. The first step is the Pharmaceutical Value Assessment.
Trusted by pharma & sciences leaders.
A selection of the pharma & sciences companies we have served.

If you're the CEO
Connect growth and margin priorities to a credible plan for patient supply and qualified capacity.
If you're the COO
Align procurement, manufacturing, quality, laboratories and distribution around released product.
If you're the Private equity operating partner
Underwrite operational value with explicit qualification costs, implementation dependencies and quality safeguards.
What's changing in pharma & sciences
Where qualified supply falls short of demand
Strategy sets the ambition. Supply chain and operations decide whether it shows up in EBITDA, cash and growth. This is Total Value Optimization™ applied to your sector.
Pricing pressure changes the supply equation
US drug-pricing negotiations and payer pressure sharpen margin scrutiny. Product-level decisions must account for supply continuity, manufacturing economics and patient access.
A second supplier is not instant capacity
API and excipient concentration creates exposure, but technical transfer, qualification and regulatory requirements constrain how quickly alternatives become usable.
Release capacity limits growth
More production can increase queues in laboratories, documentation review and deviation investigation. Rated equipment capacity can overstate the volume available for shipment.
Specialized networks need tighter coordination
CDMO dependencies, temperature-sensitive products and cross-border uncertainty complicate planning. Inventory must be evaluated by release status, shelf life and actual usability.
Illustrative example
Three different shortfalls that look the same on a report
Supplier shortage
An API or packaging supplier cannot deliver. The fix is in sourcing, and depends on how much capacity each qualified alternate really has.
Testing queue
Batches are made but waiting in the lab. Adding production makes this worse; the fix is lab capacity and scheduling.
Release delay
Testing is complete but documentation or quality disposition is pending. The fix is review flow, not more batches or suppliers.
Before qualifying an alternate, check whether it has capacity for your volume. Separating the three shortfalls stops teams fixing the wrong one.
Where the value sits
Pharmaceutical manufacturing capacity, from batch to release
Plan
Plan through release
Reconcile demand, shelf life, manufacturing slots, testing capacity and quality review in an integrated supply plan.
Buy
Build usable supplier options
Evaluate APIs, excipients, packaging and outsourced services against qualification requirements, shared upstream dependencies and total cost.
Make
Balance the batch pathway
Address campaign design, changeovers, maintenance, laboratory workload and documentation readiness without bypassing approved controls.
Move
Preserve product integrity
Align qualified lanes, temperature controls, customs documentation and logistics partners with product-specific requirements.
Fulfill
Allocate released, usable stock
Connect batch disposition, market eligibility, expiry exposure and customer priorities to distribution decisions.
Illustrative example
Follow one batch from supply to allocation
Pharmaceutical consulting that only looks at the production line misses most of the lead time. Follow one batch end to end.
01 / API and packaging supply
The batch can only start when qualified API and approved packaging components are both on hand.
02 / Testing
Once made, the batch joins the lab queue for release testing alongside every other batch.
03 / Release
Quality reviews records and test results and authorizes disposition. Only then is the batch released capacity.
04 / Allocation
Released product is allocated across markets and customers by promise date and remaining shelf life.
Your entry point
Pharmaceutical Value Assessment
Find the constraints between qualified supply and released product through Total Value Optimization™ (TVO™), Maine Pointe's end-to-end method.
Request the Pharmaceutical Value AssessmentSupply exposure map. A product-level view of supplier concentration, upstream dependencies and feasible qualification pathways.
Released-capacity baseline. A constraint assessment spanning manufacturing, testing, documentation and quality disposition.
Inventory and economics review. A view of stock usability, expiry exposure, conversion costs and resilience investment choices.
Governed implementation roadmap. Prioritized actions with accountable owners, quality decision gates and finance-reviewed value assumptions.
Illustrative example
Is it a supply shortage or a testing queue?
Supply exposure map
Shows which products depend on a single supplier, constrained upstream material or an alternate that is not yet qualified.
Released-capacity baseline
Shows how much product actually clears testing and release each period, and where batches wait.
Reading the two together tells you whether a missed order needs sourcing action or release-flow action, before money is spent on either.
Combined Intelligence / Human-led. AI-enabled.
Spotting release queues without bypassing Quality
Through Maine Pointe's Combined Intelligence model, experienced operators and governed AI work side by side. Your people make the final call, and the TVO Control Tower™ keeps the gains visible after we leave.
Illustrative example
A planner uses an alert to anticipate release delays
01
AI compares batches in testing with lab capacity and historical review times and flags orders likely to miss their release date.
02
The planner sees the alert days ahead and checks which customers and markets are affected.
03
The planner adjusts allocation and raises the queue with Quality and the lab, without changing any test or review step.
04
Quality team retains full batch-release authority. Every decision and its owner are recorded.
01 / Supplier resilience
Reveal hidden concentration
Maine Pointe's Combined Intelligence model is human-led, AI-enabled. It can organize supplier and material evidence to flag shared upstream dependencies. Procurement and quality leaders approve the qualification strategy.
02 / Capacity
Anticipate release queues
Analyze batch milestones, laboratory demand and review backlogs to surface likely constraints. Manufacturing and quality leaders make final scheduling and disposition decisions; the TVO Control Tower™ can support exception visibility.
03 / Operating knowledge
Support controlled problem solving
Maine Pointe Atlas supports retrieval of approved operating knowledge. AI can help organize recurring loss patterns, but authorized process owners validate recommendations through applicable quality controls.
Featured success stories / Pharma & Sciences
Client results and related reading
 Pharmaceutical
 company
Driving competitive global growth through strategic procurement
Closed competitive gap by 10% to 45%.
Read the client story Pharmaceutical
 company
Boosting performance and ROI quickly for a PE firm’s newly acquired company
$50M of cost take out in year one, exceeding original $25M - $41M estimate.
Read the client story Private Capital
Portfolio company
Improving performance post-carve out to boost profitability and operational efficiency
14.4% improvement in gross profitability.
Read the client storyInsights / Pharma & Sciences
Thinking for pharma & sciences leaders.
Pharma & Sciences
Pharma supply resilience: dual sourcing without doubling cost
A second supplier creates value only when its qualification, economics and upstream dependencies support a usable supply option.
Read article · 6 min
Pharma & Sciences
Capacity and compliance together: pharma operations that scale
Measure capacity through testing and release before adding equipment, shifts or inventory that the rest of the system cannot absorb.
Read article · 6 min
Pharma
U.S. Mandates to Lower Drug Pricing: Actions to Take Now
A 90-day operating playbook for pharma supply chain leaders.
Read article · 9 minYour questions, answered
Frequently Asked Questions
What does a pharmaceutical supply chain consulting firm do?
A pharmaceutical supply chain consulting firm connects sourcing, planning, manufacturing, quality release and distribution. It should improve cost and service while respecting product-specific quality and regulatory requirements.
How can pharma companies dual source without duplicating cost?
Segment materials by patient-supply risk and substitution difficulty. Compare qualification costs, minimum orders, ongoing readiness and genuinely independent supply routes before deciding where a second source is justified.
What is released capacity in pharmaceutical manufacturing?
Released capacity is how much product has cleared testing, documentation review and quality disposition and can ship by the promised date. It differs from equipment capacity because batches waiting in testing or review cannot ship.
Can procurement savings protect pharmaceutical quality?
Yes, when sourcing decisions include quality requirements and qualification dependencies from the start. Commercial savings should not assume an unapproved material, supplier or process can be used immediately.
How should pharmaceutical inventory be assessed?
Separate released stock from quarantined, market-restricted, short-dated and otherwise unusable inventory. Evaluate coverage against realistic release dates and demand, rather than counting every physical unit as available.
How does this apply to CDMO relationships?
Review reserved versus usable capacity, forecast commitments, change-control responsibilities, testing interfaces and escalation rights. A contract slot alone does not establish a reliable supply pathway.
Where should a pharmaceutical improvement program begin?
The Pharmaceutical Value Assessment maps supply exposure and released-capacity constraints. Operations, quality and finance then agree the implementation sequence, decision rights and evidence needed to validate value.
What results do pharmaceutical consulting engagements deliver?
Pharmaceutical consulting engagements are judged on measured EBITDA, cost and cash results. Published results include a 10% profitability improvement and a 10–45% competitive gap closed for a generic pharmaceutical manufacturer. Results vary by starting point, so the Pharmaceutical Value Assessment sizes your opportunity before work begins.
How long does a pharmaceutical improvement program take?
A pharmaceutical improvement program starts with the Pharmaceutical Value Assessment, which takes weeks rather than months. Implementation is phased by priority, so first savings are tracked as they land while larger changes continue over the following months.
How do you choose a pharmaceutical consulting firm?
To choose a pharmaceutical consulting firm, look for published results in your sector, people who implement alongside your teams rather than only advising, and fees tied to measured outcomes. Maine Pointe has completed 550+ engagements since 2004 and offers guaranteed performance.
Your next step / Pharmaceutical Value Assessment
Build capacity. Preserve confidence.
Guaranteed performance. Commercial terms agreed with each client.
Request the Pharmaceutical Value Assessment